Mesh lead time is not a shipping delay and it is not a queue you join. A hand-woven panel is a made-to-order textile, so the clock starts the moment a drawing is approved and stops when a keeper signs for a crate, and most of that time is spent waiting for decisions rather than for weaving. Run the order as a programme with five handoffs and the schedule becomes predictable. Run it as a purchase and the mesh arrives while the frame is still lying on the ground.
Executive Summary
A mesh lead time is decided before the loom is switched on, because four of the five handoffs in an animal enclosure order are document events and only one of them is production. The panel itself is quick in relation to everything around it; what consumes the weeks is the shop drawing approval, the pre production sample, the cutting list approval and the delivery arrangements that follow them. That is good news for a buyer, because documents can be prepared in parallel with site work, while weaving cannot be brought forward once a programme has slipped. A stainless steel rope mesh order placed without a named owner for the frame, the setting out and the unloading will still be delivered on time and will still stop the project, because an on-time crate with nowhere to be opened is not progress. The reference specification is the animal enclosure netting range product page.
Scheduling an enclosure order? Send the panel sizes, the species, the alloy and finish you need, and the date the frame will be ready. We will return a panel schedule with rope diameter, aperture, edge treatment, packing marks and the fixing allowance as a line item, plus the lead time each stage carries.
Request a panel scheduleQuick Answer:
A mesh lead time on a made-to-order panel is measured in weeks rather than days, and it is dominated by approvals rather than by weaving. Plan it as five handoffs — enquiry and drawing, sample, cutting list, packing and delivery, goods received and handover — and give each one a named owner and a date. The two things that most often extend an order lead time are a drawing that is approved late and a site that is not ready when the crate lands.
Key Takeaways
- A woven panel is made to order, so the schedule is set by approvals first and loom time second.
- Five handoffs carry the order: drawing, sample, cutting list, delivery, receiving.
- A production lead time cannot be compressed after the fact, but approval time almost always can.
- Unloading, storage and frame readiness are programme items, not details, because an unopened crate costs days.
- Every handoff needs a named owner, or the interface responsibility falls between buyer and supplier by default.
Where the material is made and by whom it is sold changes every date in that list, and the ICC, which publishes the Incoterms that fix the point where risk transfers on delivery, is the reference the delivery handoff is written against.
A Woven Panel Is Made to Order, Not Picked Off a Shelf
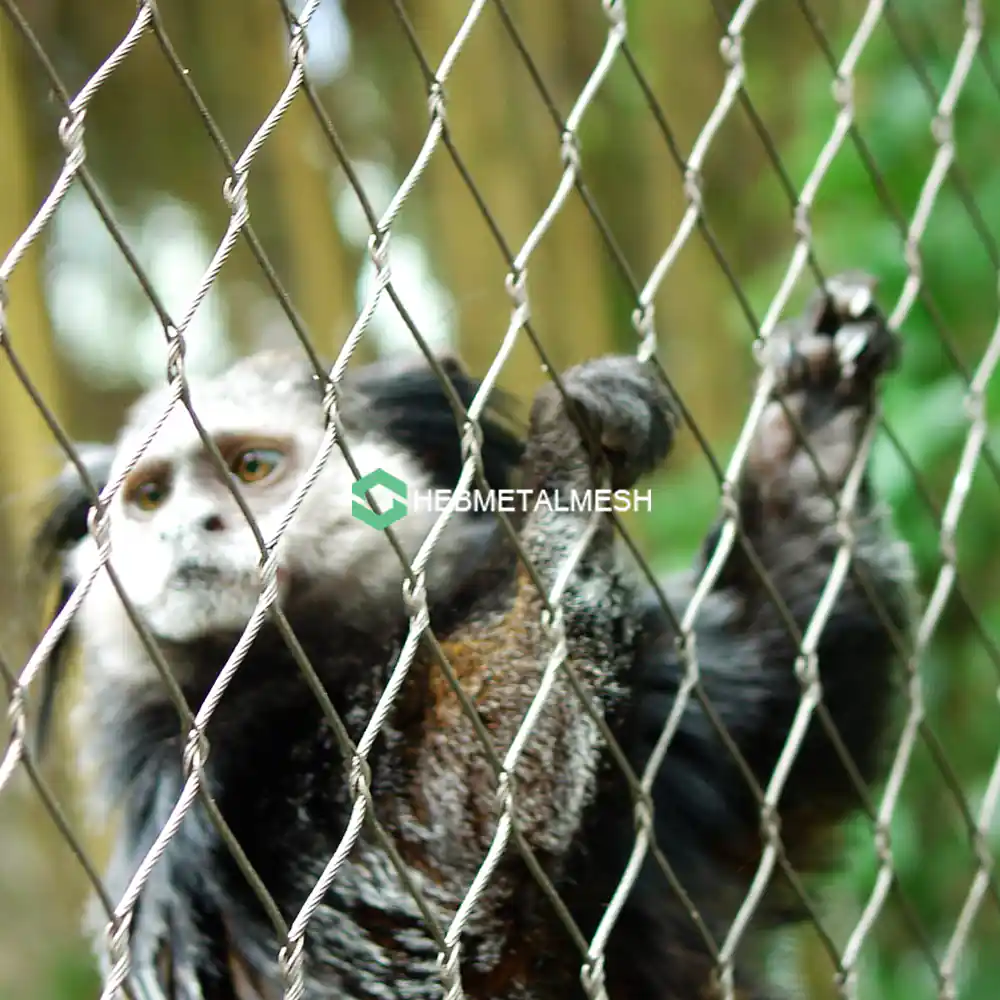
The reason a mesh lead time exists at all is that the product is not stock. A hand-woven panel is built as hand woven wire mesh — 7×7 rope, forty-nine wires inside every strand, interlaced at a fixed aperture and pitch — which is why a 3.2 mm rope at a 76 mm aperture weighs 1.5–2.0 kg/m² and why a full 9 m × 18 m sheet behaves like a sail on a lifting frame. None of that can be pulled from a rack in an arbitrary size.
So the first number to fix is whether you are buying from stock or from the loom. A standard aperture in a standard rope diameter, supplied as flexible cable netting in roll format, may sit in a warehouse with a short production lead time, and the animal enclosure mesh range works on exactly that logic: standard sizes move quickly, everything else is scheduled. A custom aperture, a specific alloy, a black oxide finish, edge cables swaged to a panel mark and a cut list that follows an out-of-square frame is a fabrication lead time measured from the day the drawing is signed, not from the day the enquiry was sent.
The weaving lead time inside that figure is the part buyers usually over-estimate. Hand weaving is labour, but it is not slow next to the paperwork around it. What actually stretches a programme is the gap between a question being asked and an answer being signed.
The Lead-Time Stack, Stage by Stage
| Stage | Owner | What has to happen before it ends |
| Enquiry and technical review | Buyer and supplier | Aperture, rope diameter, alloy, finish and format agreed |
| Drawing approval | Buyer | Shop drawing approval signed, not merely received |
| Sample | Buyer | A pre production sample or retained reference approved |
| Weaving and fabrication | Supplier | Panels woven, edges terminated, marks applied |
| Packing and freight | Supplier and forwarder | Crate built, panel marking applied, booking confirmed |
| Delivery and receiving | Buyer | Unloading planned, a goods received check completed |
Read that table as a chain and the weak links are obvious: three of the six stages end with a buyer decision, and a decision has no lead time unless somebody gives it one.
Handoffs One and Two: The Drawing and the Sample
A shop drawing approval is not an acknowledgement that the file arrived. It is a statement that the dimensions, the aperture, the rope diameter, the alloy, the finish, the edge treatment and the panel split are correct, and it is the first point at which the buyer carries the risk. Most programmes lose their first fortnight here, because the drawing is issued to somebody who is not authorised to sign it.
Expect at least one drawing revision. A woven panel is flexible, so a sloped or doubly curved bay can be approximated on the flat in more than one way, and that choice belongs to the buyer because it decides how the enclosure will look from outside. Ask for every revision to be dated and numbered, and keep the approved version on file; a programme that cannot say which revision it is building to will discover the answer at handover.
Then the pre production sample. A dated sample measured against the quoted aperture and alloy is far cheaper than a rejection in week nine, because a nominal 38 mm aperture carries a tolerance of a millimetre or two, and where a sample and a datasheet disagree the sample is the truth. Once it is approved, put it in writing that a corrosion resistant mesh reference sample is retained by both parties.
Handoff Three: The Cutting List
The cutting list approval is the quietest handoff and the one that most often turns a smooth order into a rework. A 304 stainless steel mesh panel cannot be re-cut to a smaller size without losing its terminated edge, so every panel in the schedule has to be right the first time: mark, surface, width, height, shape, aperture, rope diameter, edge treatment and quantity.
That is a geometry problem rather than a purchasing problem, and it is worth reading the panel layout guide before you sign the list, because it explains how joints are set out and why panel widths are a consequence of the bay rather than a free choice. Approve the list against a surveyed frame, not against the architect’s drawing, and photograph the bay diagonals at the same time.
Handoff Four: Packing, Delivery and Who Unloads
Panel marking is the cheapest insurance in the whole order. Every panel should arrive carrying its mark, so that unloading a container is a matching exercise rather than a puzzle, and the packing list should name panels rather than square metres. A zoo grade enclosure mesh panel is heavy enough to want two people or a lifting frame, and a crate that arrives with unmarked panels will be opened on the ground and re-stacked after lunch.
This is also the handoff where the delivery lead time stops being the supplier’s problem and becomes the buyer’s, because the point at which risk transfers is a contractual line rather than a physical one. Decide who unloads the container, whether a crane or a telehandler is booked, whether the vehicle can reach the laying-down area, and where the panels will be stored flat until the frame is ready. The packing unit itself is worth settling early: the roll and panel supply guide covers when a roll is the right format and when discrete panels are.
Handoff Five: Goods Received, Damage and Handover
The goods received check is the last moment at which a claim is easy. Open the crate with the packing list in hand, count by panel mark, measure one panel’s aperture against the approved sample, and look along the load path for damage in transit — a crushed edge cable, a kinked panel, a bent ferrule. Photograph the crate before it is opened and the damage before it is moved, and log any shortage claim the same day, because a carrier’s liability usually ends at the signature.
Then the handover review, which is a different document from the delivery note. It records what was installed, the installed cable tensioning value, the panel schedule as built and the spares held. A new woven panel beds in through its first season, so the handover review should also book the one re-tensioning visit the enclosure will need — the commissioning guide covers what a settling panel does and what to record when it settles.
Where the Responsibility Actually Sits
Every one of the five handoffs has an owner, and in a poorly run order that owner is nobody. The frame, the footings, the setting out, the base plates, the anchors and the unloading are all interface responsibility items, and each of them can be provided by you, by your contractor or by the supplier without any of those answers being wrong — provided the schedule says which.
Write the split down before the order is placed, on one page: who surveys the frame, who provides the base plates, who tensions the panels, who inspects the structure, who holds the spares. Then check that the price matches the split. Where a supplier sells mesh only and your contractor builds the frame, the supply-route guide sets out what each tier in the chain does and does not carry, so the gap in the list is visible before it becomes a delay.
What You Can and Cannot Compress
An order lead time is not one number. Approval time is elastic: pre-agree the alloy and the finish at enquiry, nominate one person with authority to sign, and answer the drawing and sample questions within days rather than weeks. Production time is only partly elastic: a standard aperture in a standard rope diameter can sometimes be pulled forward, because a hand-woven panel loses roughly 2% of a strand’s breaking load per broken wire and a batch already on the loom is genuinely interchangeable, but a bespoke finish or a swaged edge cannot be accelerated without paying for a second set-up.
Delivery lead time is the least elastic of all, and it is the one buyers forget to model. Sea freight moves on a sailing schedule, not on yours, and a crate that misses a sailing slips by weeks rather than days. Build the programme backwards from the frame-ready date with the delivery leg drawn to scale, add float at the receiving handoff rather than at the loom, and you will find that the mesh was never the slow part of the project.
Frequently Asked Questions
For a custom specification, plan in weeks rather than days, counted from drawing approval rather than from the enquiry. The loom is rarely the constraint; the drawing, the sample and the freight booking are, and each of those waits on a decision somebody has to make.
Partly. Choose a standard aperture and rope diameter, fix the alloy and finish at enquiry, nominate one signatory, and return the drawing and sample approvals in days. Production can sometimes be brought forward, but the sea leg cannot, so float belongs at the receiving end of the programme.
Whoever the order says does. Incoterms fix the point where risk and cost transfer, and that point is usually the load port for an FOB shipment, which puts unloading, inland haulage and any handling damage on the buyer’s side. Write the answer into the purchase order rather than discovering it on the quay.
Count by panel mark, measure one aperture against the approved sample, and inspect the panel edges and edge cables for transit damage. Sign only what you have counted and photographed, and raise a shortage claim the same day, because a carrier’s liability normally ends when the signature is given.